QUALITY RAW CASHEW NUT SOURCING
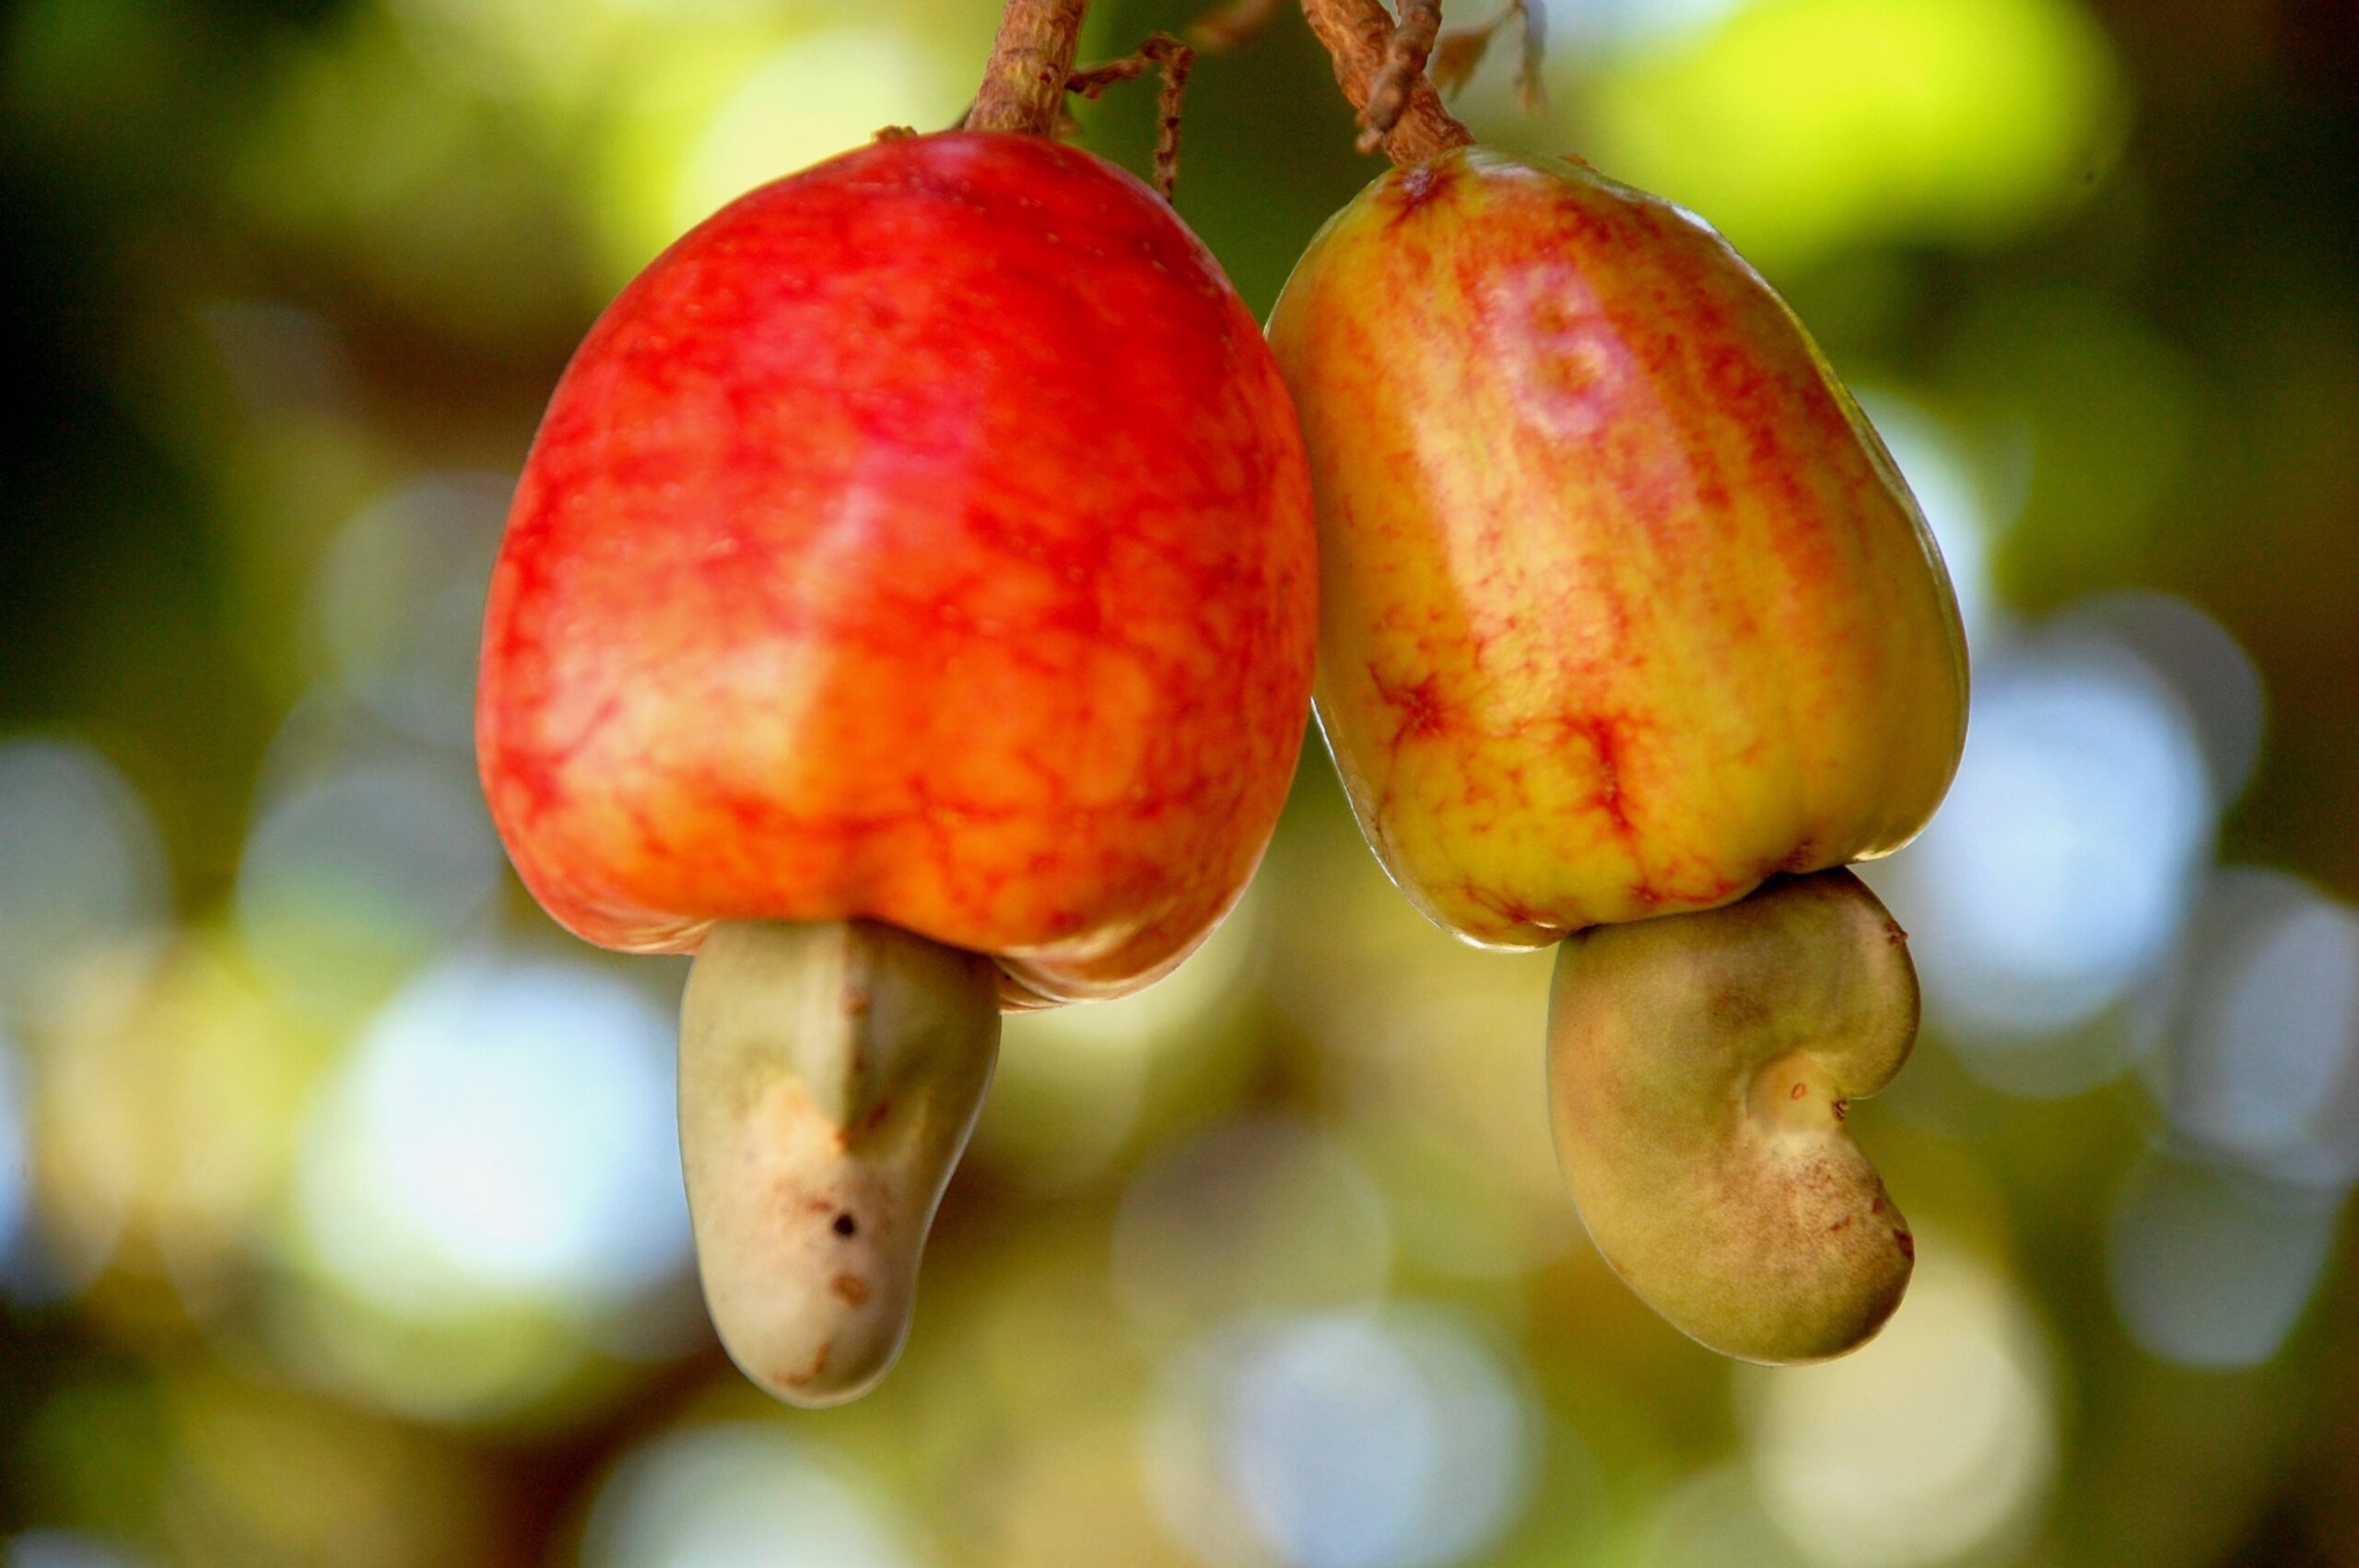
We source Raw Cashew Nuts (RCN) from Tanzania’s major cashew-producing regions, including Pwani, Lindi, and Mtwara. Our procurement approach focuses on securing high-quality, suitable raw materials that meet the requirements of our processing operations and the quality expectations of our target markets. We work within the applicable regulatory framework and adhere to the requirements, standards, and guidelines established by the Cashewnut Board of Tanzania (CBT). Through disciplined sourcing and quality-focused procurement practices, we seek to maintain a reliable supply of quality raw cashew nuts and establish strong, sustainable relationships across the supply chain.

RAW MATERIAL INSPECTION
All incoming Raw Cashew Nuts (RCN) undergo a systematic inspection and quality assessment before entering the processing stage. Our inspection process evaluates key quality parameters, including: • Moisture condition • Physical cleanliness • Nut quality and overall condition • Presence of foreign matter • Defective, immature, or damaged nuts • General suitability for processing This quality-control process helps ensure that only suitable, high-quality raw materials enter our production line, supporting consistent processing performance, product quality, food safety, and compliance with applicable standards.
CONTROLLED PROCESSING
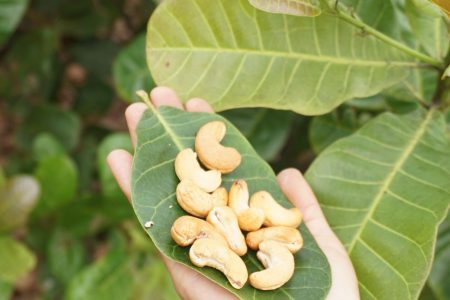
Our cashew processing operations follow a structured, multi-stage production process designed to maximize efficiency, product quality, and consistency. Key processing stages include: • Drying and preparation • Steam roasting • Cutting and shell removal • Peeling • Cleaning • Grading • Sorting Comprehensive process controls and quality checks are maintained throughout the production cycle to ensure consistent processing standards, minimize product defects, optimize yields, and produce cashew kernels that meet the quality requirements of our target markets.
KERNEL GRADING & SORTING
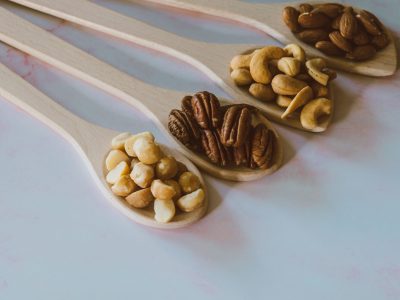
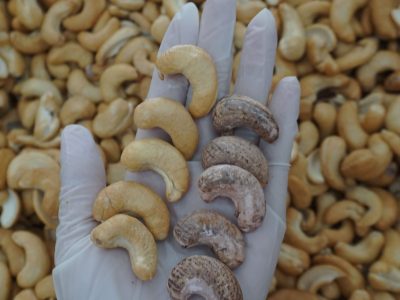
We apply a careful and systematic grading and sorting process to classify cashew kernels according to their physical characteristics, quality attributes, and specific market requirements. Our process categorizes kernels into appropriate commercial grades, including: • Whole Cashew Kernels • Cashew Pieces • White Kernels • Scorched Kernels Through disciplined grading and sorting, we aim to ensure consistent product quality, accurate classification, maximum value recovery, and compliance with customer and market specifications. This enables us to serve diverse market segments while optimizing the commercial value of our processed cashew products.
QUALITY INSPECTION OF FINISHED PRODUCTS
All finished cashew products undergo systematic quality inspection before storage, packaging, and dispatch. Our quality-control procedures are designed to identify and address defects, contamination, foreign materials, and other factors that could compromise product quality, safety, or marketability. Through rigorous final inspections and batch-level quality controls, we strive to ensure consistent quality, product integrity, and compliance with applicable standards and customer specifications across every production batch.

HYGIENIC PRODUCTION ENVIRONMENT
Our facility at Kilimahewa, Mkuranga is designed and operated to support a safe, clean, and hygienic food-processing environment. The facility comprises dedicated processing areas, quality-control facilities, storage units, secure perimeter fencing, and supporting infrastructure designed to facilitate efficient and controlled operations. We place strong emphasis on hygiene, sanitation, proper handling, and controlled storage conditions throughout the production process. These practices are intended to protect product integrity, minimize contamination risks, and maintain the quality and safety of our cashew products from processing through to final dispatch.
SAFE STORAGE & HANDLING
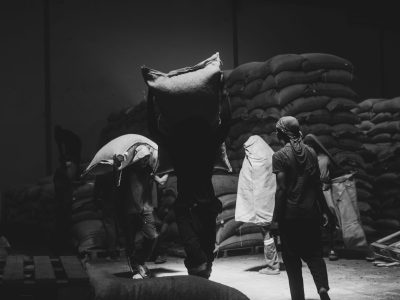
We maintain controlled handling and storage practices for both raw materials and finished cashew products to preserve their quality, safety, and integrity throughout the supply chain. Our storage and handling procedures are designed to protect products from physical damage, contamination, excessive moisture, and other environmental factors that may compromise quality. Through appropriate storage conditions, careful material handling, and systematic inventory management, we help ensure that our products remain in optimal condition from receipt of raw materials through to final dispatch.
PRODUCT CONSISTENCY
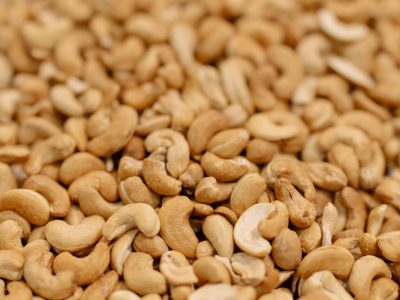
We are committed to delivering reliable and consistent cashew products that meet defined quality and customer specifications from batch to batch. Our integrated grading, sorting, inspection, and process-control systems are designed to promote uniformity in appearance, quality, size, grade, and product specifications. By maintaining disciplined quality controls throughout the production cycle, we seek to build customer confidence and establish N&F Agro Processing as a dependable supplier of consistently high-quality Tanzanian cashew products.
EXPORT-READY QUALITY
With a strategic focus on markets in the United States, European Union, and India, our quality approach is designed around the requirements of international buyers. We prepare our products with emphasis on: Product quality Consistent specifications Proper handling Hygienic processing Appropriate packaging and storage Reliable supply